Quality control & inspection
Quality problems in this trade are rarely dramatic — they are print misalignment, shade variation between panels, and frames that fail on the second season. All three are catchable before shipment if someone is looking for them. This is what we look for.
Control from material to container
Each stage has a defined output. If a stage does not produce its document or photos, the order does not move to the next one.
Material check
Fabric, ribs, shafts and components verified against the approved specification before cutting starts. Colour is compared to the reference under consistent lighting.
Pre-production sample
A sample built from bulk materials, not from stock. This is what you approve and what bulk is measured against.
First-piece check
The first units off the line are checked before the run continues, so a setting error is caught on ten pieces rather than on ten thousand.
In-line inspection
Checks during production on print registration, stitching and assembly. Problems found here can still be corrected.
Pre-shipment inspection
Finished goods sampled to an agreed AQL, with a written report and photographs sent before balance payment is due.
Loading supervision
Carton count, condition and loading sequence checked at the container. Photographs taken during loading.
What is actually inspected
A generic checklist is not enough. This is the list we work from, and you can add to it — anything you add becomes part of the standard for your orders.
| Area | Checked | Typical reference |
|---|---|---|
| Dimensions | Canopy diameter or arc, pole length and diameter, rib count, packed length | Approved specification and reference sample |
| Fabric | Composition, coating, colour against reference, shade variation between panels | GB/T 23147-2018 for canopy performance |
| Rain resistance | Canopy behaviour under controlled rainfall | GB/T 23147: (4.4 ± 0.2) mm/min for 2 min — no dripping, no water down the shaft |
| Wind resistance | Frame behaviour under load; ribs may invert | GB/T 23147: 10 m/s for 30 s with no deformation affecting use |
| UV claim | Measured, not asserted | GB/T 23147 with GB/T 18830 — UPF > 40 and UVA transmittance < 5% where claimed |
| Printing | Placement, registration, colour match, adhesion, wash and rub resistance | ISO 105-X12 rubbing, ISO 105-B02 light fastness |
| Stitching | Seam strength, skipped stitches, loose threads, panel alignment | GB/T 23147: not fewer than 15 stitches per 5 cm |
| Frame | Rib and joint condition, open and close action, wind vent function | GB 31892-2015 for safety-related retention |
| Mechanism | Crank, tilt, auto-open and closing function cycled, not just visually checked | Cycle testing; commonly 400–600 cycles for straight umbrellas |
| Corrosion | Plating and coating behaviour on metal parts | Neutral salt spray — shaft 4 h, other parts 2 h, grade 4 or better |
| Finish | Burrs, sharp edges, plating or coating defects, handle fit | EN 13830:2018 sharp edge and point test where the EU market applies |
| Packing | Quantity per carton, carton strength, marking, barcode legibility | Your packing specification and drop-test requirement |
References are the published criteria most often applied in this category. The applicable edition and any customer-specific protocol are confirmed in writing before production.
Each reference above has a defined test condition and pass threshold. See Standards & compliance for the full list, including the EU physical safety standard, US lead limits and the differences between UPF test methods.

Bench inspection — dimensions, print registration and handle fit checked against the golden sample

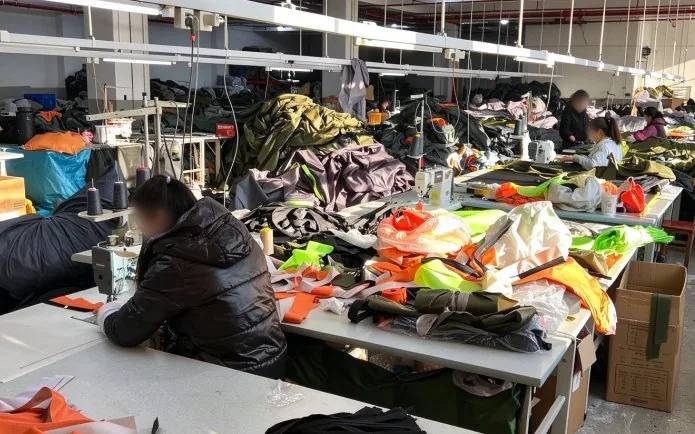
In-line checking on the sewing floor — catching a fault here costs a panel, not a container
What everything is checked against
An inspection is only meaningful if there is one agreed physical reference. Before bulk starts, the approved sample is sealed, signed and held — by us and by you — and production is judged against that piece rather than against a description.
- Sealed approval sample — one unit from the approved run, signed off and retained as the reference for production and for any later re-order.
- Golden sample copies — duplicates can be sent to you or to your inspection company, so the same reference sits on both sides.
- Colour reference — the approved lab dip travels with the order file. Bulk fabric is checked against that physical piece, since photos and screens shift colour.
- Documented tolerances — dimensions, print registration and functional checks are recorded with their tolerances in the order confirmation, not decided at final inspection.
- Re-order continuity — the sealed reference is reused for repeat programmes, which is usually what decides whether a second run matches the first.
Claims rarely come from a missed measurement. They come from a specification that was never written down — a tolerance discussed but not confirmed, or a verbal colour agreement. Everything above exists to remove that grey area while the order is still open.

Colour checked against the reference before it is sealed — see how colour is matched
The problems we see most often
Knowing the likely failure modes is what makes an inspection useful. These are the defects that most often reach a buyer when nobody checks for them.
Colour drift between panels
Panels cut from different dye lots. Caught by comparing panels side by side rather than against a reference alone.
Print misregistration
Logo off position or doubled edges, especially on multi-colour screen work. Checked at first-piece stage.
Stitching failures
Skipped stitches at the rib tips are the most common place an umbrella starts to fail in use.
Mechanism stiffness
Crank and auto-open mechanisms that work once but bind after cycling. We cycle them rather than operate them once.
Corrosion on metal parts
Most relevant for coastal and resort programmes. Material specification is the prevention; inspection is the backstop.
Carton under-strength
Cartons that arrive crushed. Checked at packing, and packing method can be specified in the order.
AQL, in plain language
AQL — acceptable quality limit — is the number of minor defects a shipment may contain before it is rejected. It exists because inspecting every unit of a ten-thousand-piece order is not practical, and because "zero defects" is not a measurable instruction.
- Critical defects — safety or function failures. Acceptance is normally zero.
- Major defects — noticeable problems that affect saleability, commonly set at AQL 2.5.
- Minor defects — cosmetic issues that most buyers tolerate, commonly AQL 4.0.
The sampling level belongs in the order, not in a discussion after inspection. Tell us the AQL you work to and we will confirm it in writing before deposit.
| Defect class | Typical AQL | Examples |
|---|---|---|
| Critical | 0 | Broken frame, sharp exposed edge, wrong safety-critical component |
| Major | 2.5 | Print misalignment, open seam, mechanism failure, wrong colour |
| Minor | 4.0 | Loose thread, small mark, slight variation within tolerance |
Commonly used levels shown as a starting point. Your AQL is set by your requirements and confirmed in the order.
Third-party inspection and testing
For a first order with a new supplier, or any order large enough that a failure would be expensive, an independent inspection is worth the fee. We arrange it and share the report whether it is favourable or not.
Pre-shipment inspection
An independent inspector samples the finished goods to your AQL. Cost typically a few hundred US dollars per man-day, borne by the buyer.
Laboratory testing
Fabric composition, colour fastness, UV performance, water column or restricted substances, to the standard your market requires. Options include ISO 811 for water resistance, the ISO 105 series for colour fastness, ISO 9227 salt spray, and OEKO-TEX Standard 100 for chemical content.
During production
In-line visits when a long run or a new model justifies checking before the goods are finished and packed.
Inspection finds problems; it does not prevent them. On a first order the strongest controls are a written specification, an approved reference sample, and a factory that has made the item before. We prioritise those before inspection.
If something is wrong
How a claim is handled matters more than a promise that nothing will go wrong. This is our sequence.
Evidence
Send photographs showing the defect, the quantity affected and the carton or batch reference. We need it within an agreed window after arrival.
Assessment
We compare against the approved reference sample and the inspection report to establish what happened and where.
Resolution
Depending on the finding: replacement parts, Credit against the next order, or re-production. Agreed in writing.
Prevention
The specification or inspection checklist is updated so the same defect does not reach you twice.
The last hand check
Before a canopy goes onto a frame it is folded, checked and finished by hand. Folding marks and seam alignment are the two things an inspector looks for.

Folding and finishing — the last hand check before assembly
Tell us the standard you need
Send your AQL, inspection requirements or testing standards and we will confirm what we can meet and what it costs.
Discuss quality requirements